
Overview: Understanding Cylinder Configuration Options
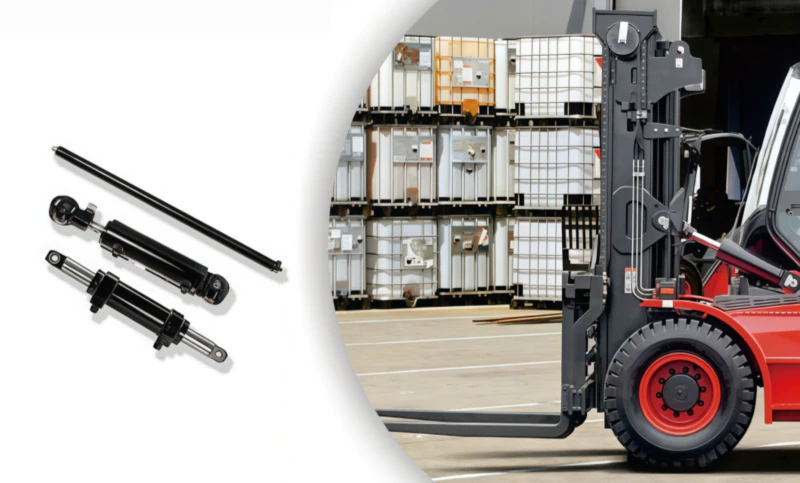
The fundamental difference between double-acting and single-acting tilt cylinders lies in how they generate force: double-acting cylinders produce controlled force during both extension (tilting backward) and retraction (tilting forward) phases, while single-acting cylinders generate force during extension only, relying on gravity or spring force for retraction. This architectural difference creates profound impacts on performance, safety, reliability, cost, and operational characteristics that influence equipment design and selection decisions across warehouse and industrial applications.
Most modern industrial forklifts (80%+ of counterbalance and reach equipment in active use) employ double-acting tilt cylinders, which provide superior control, faster response, smoother operation, and enhanced safety characteristics compared to single-acting designs. However, single-acting cylinders remain common in specialized applications, particularly on small pallet jacks, lightweight stackers, and specialized load-handling equipment where cost minimization and simplicity outweigh performance advantages. Understanding the technical differences, performance trade-offs, and application-specific strengths of each design enables equipment engineers and maintenance managers to make informed selection decisions aligned with specific operational requirements.
Double-Acting Cylinder Design and Operation
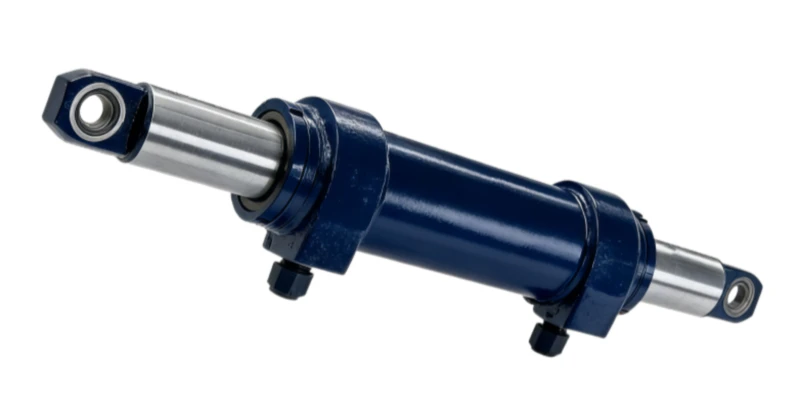
Double-acting cylinders feature piston rods that respond to hydraulic pressure in both directions: pressurized fluid supplied to the extend port forces the piston forward (and mast backward into tilt-back position), while pressurized fluid supplied to the retract port pulls the piston rearward (and mast forward into tilt-forward position). Both directions require active hydraulic pressure to achieve controlled force output and speed regulation.
Key Double-Acting Cylinder Characteristics:
Dual Port Configuration: Four hydraulic ports (extend inlet/outlet and retract inlet/outlet, or two main ports each with pilot line access) enable independent pressure regulation in both directions. This dual-circuit architecture allows separate control valve optimization for extension and retraction speeds, enabling fine-tuned mast positioning across the full tilt range.
Pilot-Operated Check Valves: Integrated check valves in each end cap prevent pressure loss and maintain mast position when controls are neutral. Without these check valves, internal seal leakage would cause gradual mast drift. These precision valves require cleanliness standards (ISO 17/15/12 or finer) and add $400-$600 to cylinder manufacturing cost, but provide essential load-holding capability in double-acting systems.
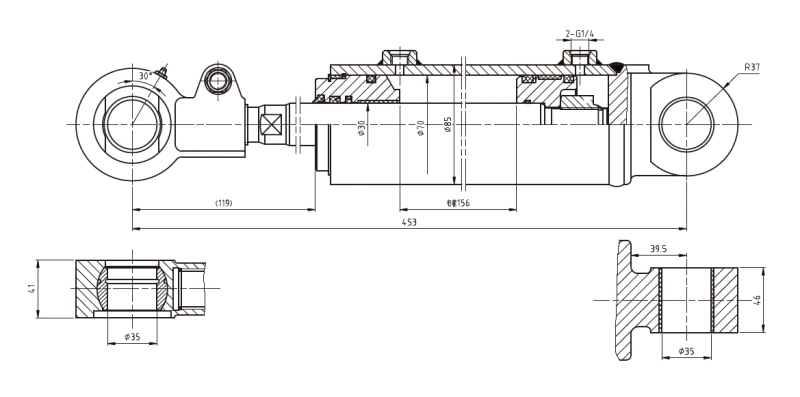
Extended Rod Design: Double-acting cylinders typically feature larger rod diameters (often 0.6-0.7 times bore diameter) compared to single-acting cylinders, providing greater mechanical strength and bending resistance. The larger rod accommodates load forces generated during retraction phases and provides stiffness during mast lowering operations under full load.
Performance Characteristics: Extension and retraction speeds can be independently controlled through separate flow regulation, enabling smoother load positioning and operator-friendly response characteristics. Mast position under load is actively maintained through pilot-operated check valves rather than relying on friction or gravity, providing stable positioning even when subject to vibration or side loads.
Single-Acting Cylinder Design and Operation
Single-acting cylinders feature a piston rod that extends when pressurized fluid enters the cylinder but relies on gravity or spring force for retraction. Only the extend port requires hydraulic pressure; the retract port is vented to the reservoir or atmosphere. This simpler design reduces component complexity, hydraulic circuit requirements, and manufacturing cost compared to double-acting systems.
Key Single-Acting Cylinder Characteristics:
Single Port with Spring Return: Pressurized fluid enters through one port to extend the piston, while a return spring provides retraction force. Spring preload determines the extension force threshold—when hydraulic pressure drops below spring force, the cylinder retracts. This self-contained design eliminates need for separate retract-phase pressure supply and pilot-operated check valves.
Gravity-Dependent Positioning: On tilt applications, gravity assists retraction when the mast tilts forward (lowering the rear). On equipment mounted vertically or with tilting angles exceeding 30 degrees forward, gravity alone may provide insufficient retraction force, requiring stiffer return springs or auxiliary hydraulic assist. This gravity-dependency creates consistency challenges: retraction speed varies based on load weight and mast angle.
Reduced Rod Diameter: Single-acting cylinders typically feature smaller rod diameters (0.4-0.5 times bore diameter) since retraction force is primarily supplied by springs or gravity rather than hydraulic pressure. This reduced rod size lowers manufacturing cost and material expense but provides less resistance to bending stresses during use.
Cost and Simplicity Advantages: Single-acting design reduces manufacturing complexity, requires fewer hydraulic ports and connections, eliminates pilot-operated check valve complexity, and typically costs 30-40% less than equivalent double-acting cylinders. The simpler design appeals to cost-conscious equipment manufacturers targeting price-sensitive markets (small pallet jacks, basic stackers, rental equipment fleets).
Limitations: Single-acting cylinders cannot provide controlled retraction force—mast descent speed is determined by spring stiffness and gravity, not operator control. Load-holding under vibration or side loads relies on friction and spring preload rather than active hydraulic pressure, potentially allowing gradual position drift. Operator control over descent speed is limited or absent, reducing positioning precision.
Performance Comparison: Speed, Control, and Precision
Double-acting cylinders typically achieve full tilt cycles (backward to forward positioning) in 8-12 seconds, with extension and retraction speeds independently controlled through separate valve circuits. Retraction speed under load can be deliberately slowed for precision positioning, while extension can be optimized for rapid mast adjustment. Operators experience smooth, controlled response that matches input pressure smoothly with output speed.
Single-acting cylinders operate at 15-25 seconds for full tilt cycles, with retraction speed fixed by spring characteristics and gravity. Once the operator releases the tilt control, retraction begins immediately at the fixed spring-determined speed—no gradual deceleration or speed adjustment capability exists. This all-or-nothing characteristic makes single-acting systems less operator-friendly for precise positioning and creates potential control issues when operators must coordinate load placement with fixed descent speeds.
Load Positioning Precision: Double-acting systems enable smooth load positioning through partial control valve actuation and proportional flow regulation. Operators can position masts incrementally—opening valves partially to control descent speed, allowing fine adjustments and smooth load placement. Single-acting systems lack this control—partial valve opening provides no speed control during retraction (springs provide the retraction force regardless of valve position), forcing operators to choose between “fully extended” and “fully retracting” without intermediate speeds.
Safety and Reliability Characteristics
Double-acting cylinders provide superior safety through active mast positioning and load-holding capability. Pilot-operated check valves maintain mast position even when the hydraulic system is deactivated, preventing uncontrolled mast descent when hydraulic failure occurs. This fail-safe characteristic is critical in high-traffic warehouse environments where unexpected mast movement could create injury hazards or load instability.
Single-acting cylinders rely on spring preload and friction to maintain load position. During hydraulic system failure (pump shutdown, hose rupture), springs immediately retract the cylinder regardless of operator input. On horizontal tilt applications, this spring-forced retraction is generally safe. However, on vertically-mounted or extreme-angle equipment, uncontrolled spring-forced retraction can create hazardous situations if loads are not properly secured or if operators are positioned beneath suspended loads.
Maintenance Requirements: Double-acting cylinders require more sophisticated maintenance: pilot-operated check valves must be kept clean (ISO 17/15/12 or finer fluid cleanliness) to function properly, seal kits typically cost $300-$500 compared to $100-$150 for single-acting systems, and pressure testing procedures are more complex due to independent circuit verification requirements. However, the superior control and positioning precision reduce operator error and damage risk, often offsetting higher maintenance costs through better equipment protection.
Single-acting cylinders require minimal maintenance—springs are non-critical to regular servicing, seal replacement is straightforward ($100-$150), and no pilot-operated components require specialized fluid cleanliness. However, spring degradation over time (springs weaken with age, reducing retraction force) gradually degrades performance, and there is no practical field maintenance option—tired springs require cylinder replacement.
Cost Analysis: Acquisition, Maintenance, and Lifecycle Considerations
Double-acting cylinders cost $3,500-$5,000 for standard industrial sizes, while equivalent single-acting cylinders cost $2,100-$3,200—approximately 30-40% less acquisition cost. This cost difference reflects pilot-operated check valve complexity, larger rod sizing, and dual-circuit design requirements in double-acting systems.
However, 5-year total cost of ownership analysis typically favors double-acting cylinders despite higher acquisition costs. Double-acting systems experience lower failure rates (seal degradation reduced through better load control and less vibration stress), longer component lifespan (pilot-operated check valves properly maintained last 5+ years compared to springs degrading within 3-4 years), and reduced maintenance emergency costs (fewer unplanned failures reduce emergency service expenses). Comprehensive TCO analysis typically shows $800-$1,500 per-unit advantage for double-acting systems over 5-year lifecycle compared to single-acting alternatives.
Total Cost of Ownership Comparison (5-year period):
Double-Acting: Acquisition: $4,200. Maintenance (seal kit replacement, pilot valve service): $1,200. Emergency repairs (1 failure event): $2,500. Downtime costs (lower failure rate): $1,000. Total: $8,900 per cylinder.
Single-Acting: Acquisition: $2,800. Maintenance (seal replacement): $600. Emergency repairs (2 failure events, spring degradation): $5,200. Downtime costs (higher failure rate): $2,500. Total: $11,100 per cylinder.
5-year advantage for double-acting cylinders: $2,200 per unit, or $44,000 on a 20-forklift fleet.
Application-Specific Selection Criteria
Equipment selection should consider specific application requirements when choosing between double-acting and single-acting designs. High-performance warehouse environments with frequent load handling, precision positioning requirements, and continuous operation favor double-acting cylinders despite higher cost—superior control and reliability justify investment through improved productivity and reduced downtime.
Double-Acting Selection Criteria: High-utilization equipment (>70% operating time), environments requiring frequent load positioning adjustments, precision loading applications (stackable pallets, fragile goods), mixed-duty equipment serving multiple load types and configurations, facilities with limited spare equipment availability (downtime impact is critical), and safety-critical applications where load-holding during power loss is essential.
Single-Acting Selection Criteria: Low-utilization equipment (rental fleets, backup equipment, seasonal use), simple load handling (single-height positioning, fixed load types), budget-constrained operations prioritizing acquisition cost minimization, applications where mast descent speed consistency is not critical, and equipment where spring retraction characteristics match operational requirements (minimal load variation, moderate descent distances).
Equipment Conversion and Retrofit Considerations
Converting equipment from single-acting to double-acting cylinders requires more than simple component replacement—it demands control system reconfiguration and hydraulic circuit redesign. Single-acting equipment typically uses simple selector valves routing pressure to extend port only; converting to double-acting requires proportional directional control valves with separate extend and retract circuits, addition of pilot-operated check valve circuits, and integration of new hydraulic lines and pressure relief valve configuration.
Full conversion typically costs $3,500-$6,000 in hydraulic system modifications beyond the cylinder replacement cost, making retrofit economically justified only for high-value equipment or critical applications. For most facilities, accepting equipment’s original design specification remains more economical than attempting mid-life conversion to alternative cylinder architecture. However, conversion can be justified when retrofitting aging single-acting equipment to extend lifespan and improve positioning precision for changing operational requirements.
Professional Selection and Specification Support
Selecting appropriate cylinder architecture requires careful evaluation of operational requirements, budget constraints, and lifecycle cost considerations. Tiltcylinder.net’s engineering team can assist with selection analysis, cost-benefit comparisons, and retrofit feasibility assessment for existing equipment. Our technical consultants review your specific application requirements and provide data-driven recommendations balancing performance, reliability, and total cost of ownership.
Contact our engineering team with your equipment specifications and operational requirements, and we’ll provide detailed selection recommendations tailored to your specific needs. Visit our resource center for additional technical documentation and specification comparison tools. For integrated hydraulic system design guidance, explore compatible bearing systems documentation for complete equipment architecture planning.
Conclusion: Strategic Selection for Optimal Performance and Value
Double-acting and single-acting tilt cylinders represent fundamentally different design philosophies: double-acting prioritizes control, precision, reliability, and load-holding capability for professional warehouse operations, while single-acting emphasizes simplicity, cost minimization, and basic functionality for cost-conscious or light-duty applications. Neither design is universally superior—each excels in specific applications aligned with their design strengths and operational characteristics.
For high-performance warehouse environments, frequent load handling, and professional operations where downtime costs are significant, double-acting cylinders deliver superior return on investment despite higher acquisition cost through improved reliability, precision control, and extended component lifespan. For budget-constrained operations, light-duty equipment, and applications where simplicity and cost minimization dominate selection criteria, single-acting cylinders remain practical options that accomplish fundamental load handling functions economically. Understanding the technical differences, performance trade-offs, and application-specific strengths of each design enables informed selection decisions that optimize overall equipment performance and economic value for your specific operational requirements.


